追求卓越品质 创造世界品牌
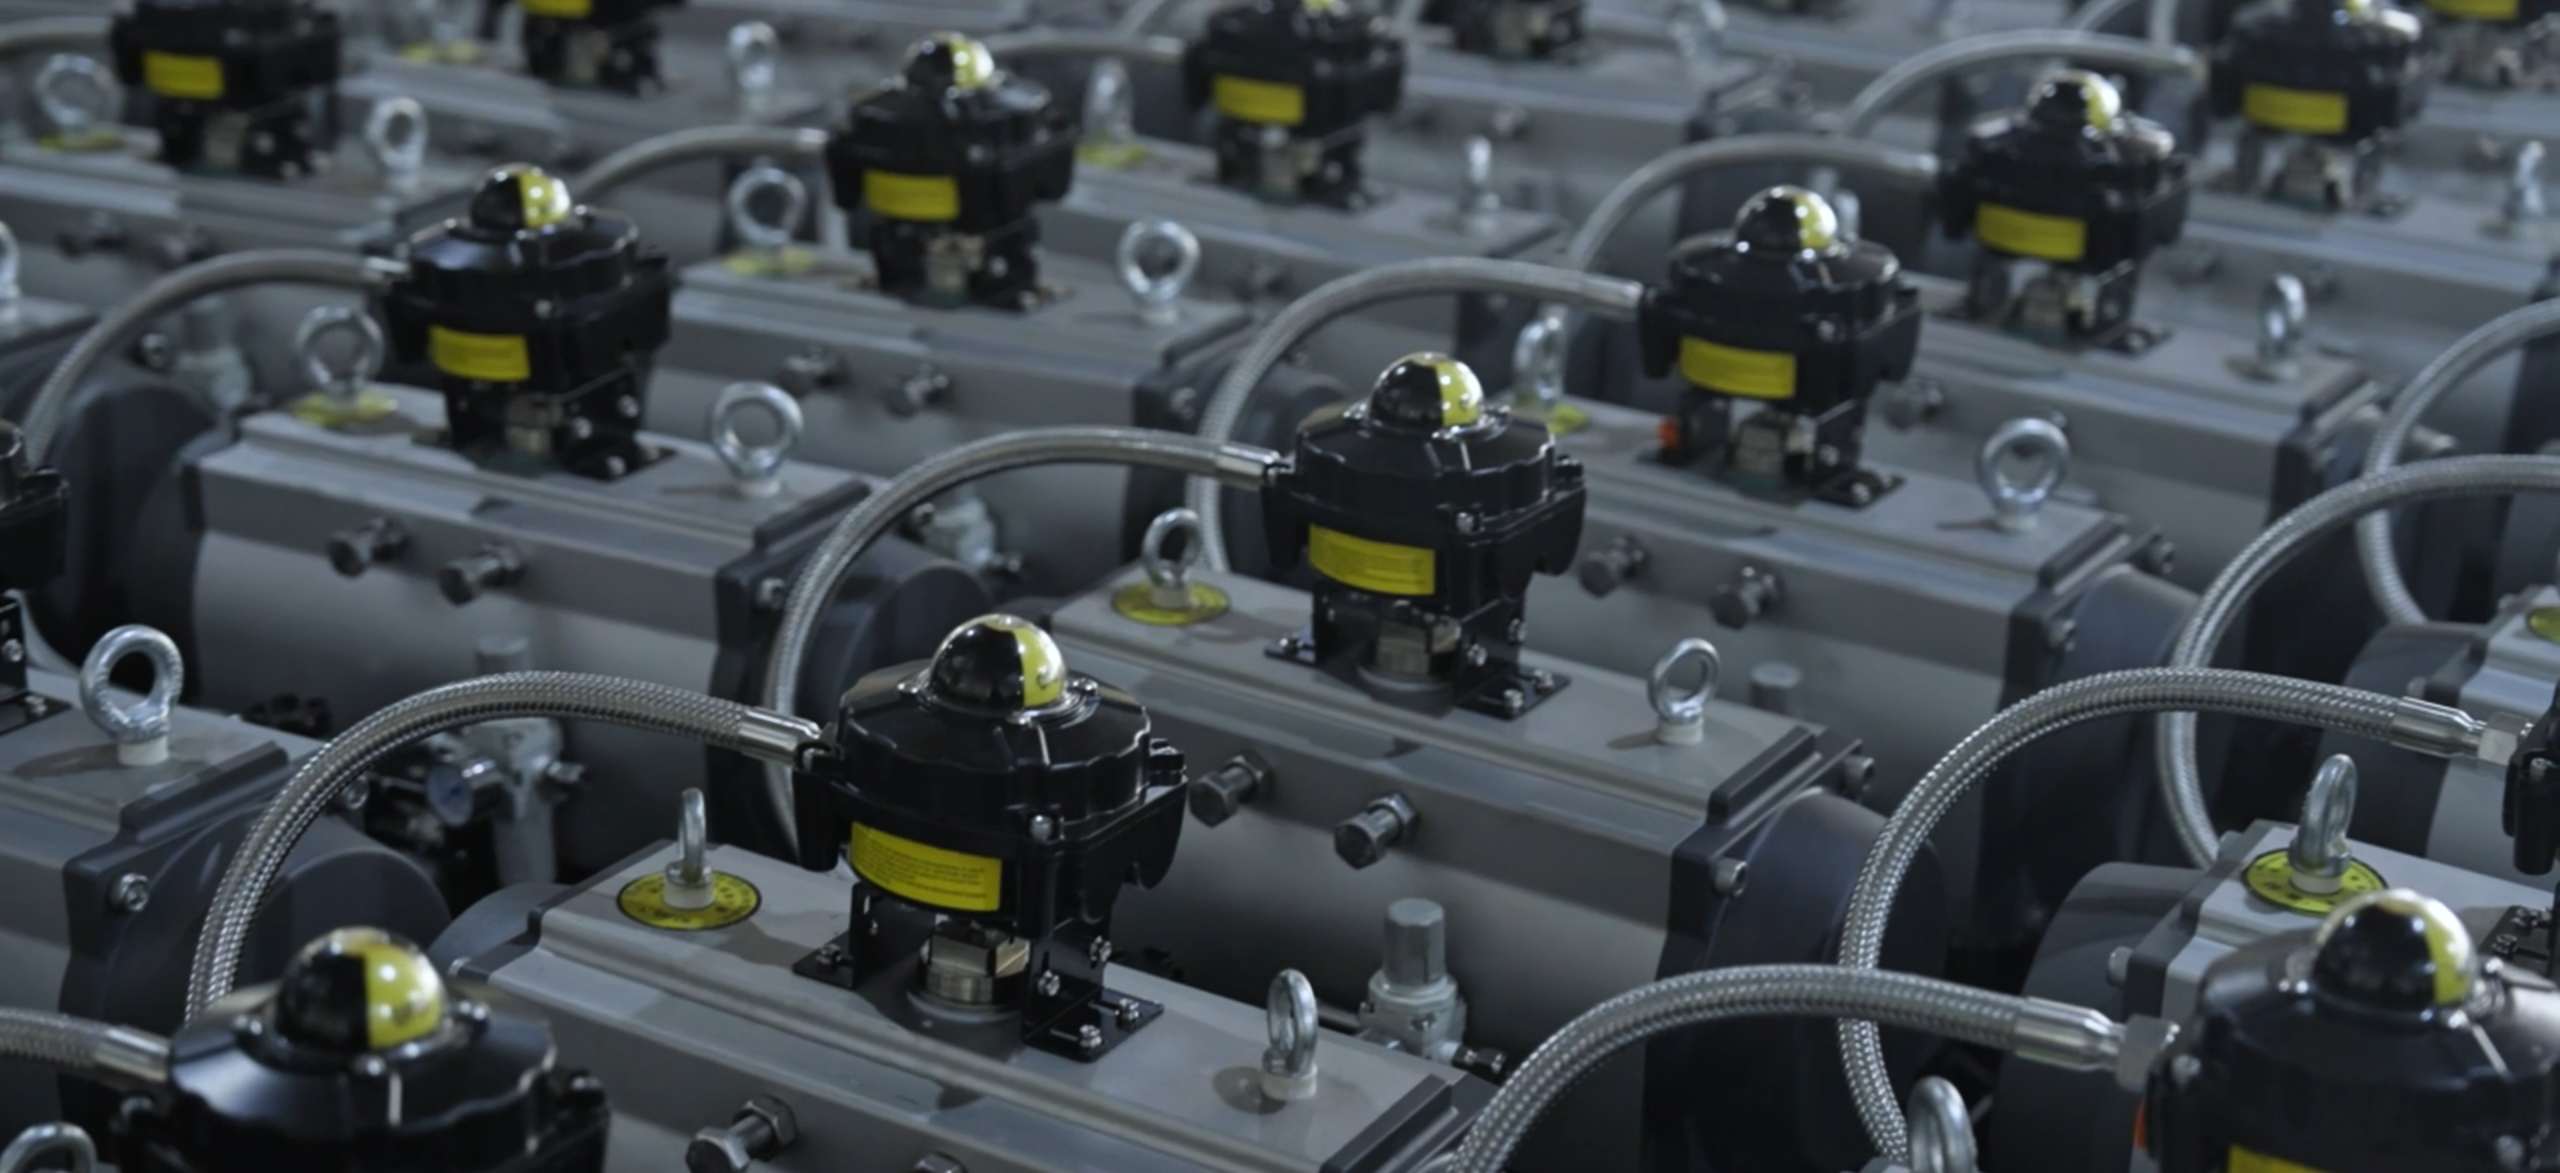


Hangda Top Mounted Ball Valve: Ushering In A New Era Of Efficient Fluid Control
In medium high pressure and large-diameter pipeline systems, ball valves play an important role in cutting off and regulating the flow of media as key control components. Hangda Valve Group Co., Ltd. has been deeply involved in the field of industrial valves for many years. Combining mature manufacturing capabilities and understanding of working conditions, we have launched multiple series of top mounted ball valve products, which are widely used in industries such as oil and gas, chemical, power, municipal, etc., to meet customers' equipment needs for high reliability, easy maintenance, and long service life.

Upper structure design to improve maintenance efficiency
The upper mounted ball valve of Hangda adopts a top maintenance structure, which can complete online maintenance of internal components such as the ball, sealing seat, and valve stem without dismantling the entire pipeline, greatly reducing operation and maintenance costs and downtime. The product is designed with multiple integrated valve bodies, reducing flange connections, enhancing pressure bearing capacity, and reducing the risk of leakage. The valve structure integrates anti blowout valve stem, fireproof sealing, and anti-static devices, effectively ensuring the safety of equipment in critical working conditions such as high temperature, high pressure, and flammability.


Multi industry application, adaptable to complex working conditions
Thanks to its excellent sealing performance and structural stability, the Hangda top mounted ball valve is widely used in multiple industry scenarios. In the oil and gas pipeline system, it is suitable for core nodes such as oil transfer stations, gate stations, and LNG terminals; In the chemical industry, it is capable of safely cutting off and controlling corrosive, toxic, or high viscosity media; In power plants and municipal heating projects, it has excellent pressure and temperature resistance performance, meeting high-frequency opening and closing requirements such as hot water and steam. A variety of sealing forms and valve body Material can be selected, which is convenient for flexible adaptation to different media environments.

Stable manufacturing standards to ensure product consistency
Hangda Valve strictly adheres to international standards such as API 6D, ASME B16.34, and API 598. The products have passed standardized inspection processes in terms of structural dimensions, sealing testing, and pressure performance. The company has a comprehensive production and quality control system, which ensures that every upper mounted ball valve meets long-term operating standards and provides customers with stable and reliable fluid control solutions, from raw material entry, part processing to complete machine testing, with layers of checks.
As an important force in domestic industrial valve manufacturing, Hangda Valve Group Co., Ltd. will continue to adhere to technology driven and quality assurance, continuously improve the reliability, adaptability, and service response capabilities of upper mounted ball valve products, provide more efficient and safe pipeline control support for various industries, and assist users in stable system operation and long-term project development.
 Previous News

Hangda Top Mounted Ball Valve: Ushering In A New Era Of Efficient Fluid Control
In medium high pressure and large-diameter pipeline systems, ball valves play an important role in cutting off and regulating the flow of media as key control components. Hangda Valve Group Co., Ltd. has been deeply involved in the field of industrial valves for many years. Combining mature manufacturing capabilities and understanding of working conditions, we have launched multiple series of top mounted ball valve products, which are widely used in industries such as oil and gas, chemical, power, municipal, etc., to meet customers' equipment needs for high reliability, easy maintenance, and long service life.
Upper structure design to improve maintenance efficiency
The upper mounted ball valve of Hangda adopts a top maintenance structure, which can complete online maintenance of internal components such as the ball, sealing seat, and valve stem without dismantling the entire pipeline, greatly reducing operation and maintenance costs and downtime. The product is designed with multiple integrated valve bodies, reducing flange connections, enhancing pressure bearing capacity, and reducing the risk of leakage. The valve structure integrates anti blowout valve stem, fireproof sealing, and anti-static devices, effectively ensuring the safety of equipment in critical working conditions such as high temperature, high pressure, and flammability.
Multi industry application, adaptable to complex working conditions
Thanks to its excellent sealing performance and structural stability, the Hangda top mounted ball valve is widely used in multiple industry scenarios. In the oil and gas pipeline system, it is suitable for core nodes such as oil transfer stations, gate stations, and LNG terminals; In the chemical industry, it is capable of safely cutting off and controlling corrosive, toxic, or high viscosity media; In power plants and municipal heating projects, it has excellent pressure and temperature resistance performance, meeting high-frequency opening and closing requirements such as hot water and steam. A variety of sealing forms and valve body Material can be selected, which is convenient for flexible adaptation to different media environments.
Stable manufacturing standards to ensure product consistency
Hangda Valve strictly adheres to international standards such as API 6D, ASME B16.34, and API 598. The products have passed standardized inspection processes in terms of structural dimensions, sealing testing, and pressure performance. The company has a comprehensive production and quality control system, which ensures that every upper mounted ball valve meets long-term operating standards and provides customers with stable and reliable fluid control solutions, from raw material entry, part processing to complete machine testing, with layers of checks.
As an important force in domestic industrial valve manufacturing, Hangda Valve Group Co., Ltd. will continue to adhere to technology driven and quality assurance, continuously improve the reliability, adaptability, and service response capabilities of upper mounted ball valve products, provide more efficient and safe pipeline control support for various industries, and assist users in stable system operation and long-term project development.
Previous News
CopyRight©2018 Valve Data Center All rights reserved
customer service hotline:400-633-5118/86-0577-86857700
Valve Data Center - Chinese Valve Service Media, Empowering Global Industrial Safety.

客服

微信公众号

关注抖音号

苹果App

华为App


